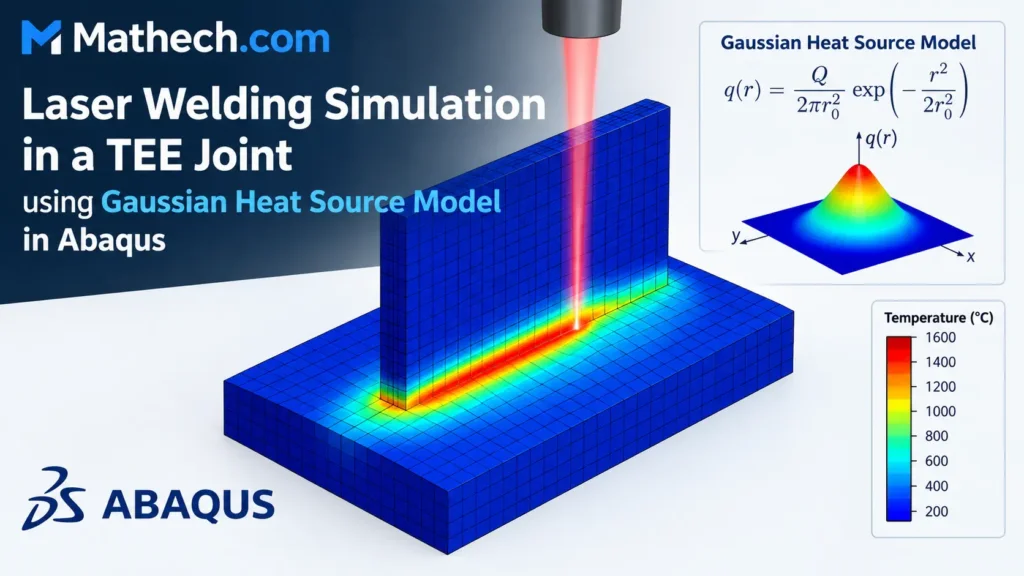
Pulsed laser welding delivers laser energy in controlled on–off cycles rather than as a continuous beam. This changes the thermal cycle, weld-pool behavior, penetration, and heat-affected zone.
For numerical welding simulation, the pulse must be represented as a time-dependent heat source. A constant laser power is not equivalent to a pulsed laser, even when both processes have the same average power.
This article provides a practical framework for modeling pulsed laser welding, including pulse energy, frequency, pulse width, duty cycle, average power, peak power, heat-source equations, temperature-dependent material properties, latent heat, and Abaqus DFLUX implementation.
1. Pulsed Laser Welding Parameters
A pulsed laser is defined by several parameters that must be kept separate in both experiments and simulations.
The main parameters are:
| Parameter | Symbol | Unit | Meaning |
|---|---|---|---|
| Peak laser power | Ppeak | W | Laser power during the pulse |
| Pulse duration | ton | s | Duration of each laser pulse |
| Pulse period | T | s | Time between the start of consecutive pulses |
| Frequency | f | Hz | Number of pulses per second |
| Duty cycle | D | % | Fraction of time the laser is ON |
| Pulse energy | Ep | J | Energy delivered during one pulse |
| Average power | Pavg | W | Time-averaged laser power |
| Absorption efficiency | η | — | Fraction of laser power absorbed by the material |
f
T
2- Simulation Strategy for Pulsed Laser Welding in Abaqus
A reliable pulsed laser welding simulation in Abaqus should be developed progressively. Do not start with the complete moving pulsed heat-source model. Build and verify each component before adding the next level of complexity.
Analytical Calculation
Start by calculating the fundamental laser parameters before creating the Abaqus model.
These calculations provide reference values for checking the numerical model later.
Static Heat-Source Test
Begin with a stationary laser heat source. Do not introduce laser movement at this stage.
Verify:
- Heat flux magnitude
- Temperature increase
- Spatial distribution of the heat source
Continuous Moving Laser
After confirming the stationary heat source, introduce laser movement while keeping the heat source continuously active.
Verify that the heat source moves along the intended welding path with the correct magnitude and velocity.
Pulsed Stationary Laser
Activate the pulse function while keeping the laser stationary. This isolates the temporal behavior of the pulsed heat source.
The temperature should show a corresponding rise during the laser-on period and cooling during the laser-off period.
Moving Pulsed Laser
Once both movement and pulsing work independently, combine them into the complete moving pulsed laser heat source.
Combine the spatial heat-source distribution with the laser position and pulse function:
The resulting model represents the time-dependent heat input during pulsed laser welding.
Material Nonlinearity
After verifying the heat-source implementation, introduce temperature-dependent material properties.
- Temperature-dependent thermal conductivity, k(T)
- Temperature-dependent specific heat, Cp(T)
- Temperature-dependent density, ρ(T)
- Latent heat near melting
Adding these effects at this stage makes it easier to identify whether numerical problems originate from the heat source or from the material model.
Experimental Validation
The final step is to compare the Abaqus prediction with experimental measurements.
3. Calculate Peak Power, Pulse Energy, and Average Laser Power
These quantities are often confused in pulsed laser welding. Understanding the difference between pulse energy and average power is essential for correctly defining the laser heat input.
For a rectangular laser pulse, the energy delivered during one pulse is:
Therefore, a 1000 W laser operating for 2 ms delivers:
Pulse energy
The laser delivers 2 J of energy during each pulse.
If the laser operates at 100 Hz, the average power is calculated from the pulse energy and pulse frequency:
Therefore:
Average laser power
The time-averaged laser power is therefore 200 W.
The same result can be obtained directly from the peak power and duty cycle:
Because the duty cycle is related to frequency and pulse duration by:
For this example:
Therefore:
4. Example of a Pulsed Laser
Consider:
- Peak power: 1000 W
- Pulse duration: 2 ms
- Frequency: 100 Hz
- Absorption efficiency: 0.8
The pulse period is calculated from the pulse frequency:
100 = 0.01 s
The duty cycle is the ratio of the pulse duration to the pulse period:
0.01 = 0.2
Duty cycle
D = 20%
The energy delivered during one laser pulse is:
Pulse energy
Ep = 2 J
The average laser power is obtained by multiplying the peak power by the duty cycle:
Average laser power
Pavg = 200 W
The average absorbed power accounts for the absorption efficiency of the material:
Average absorbed power
Pabs,avg = 160 W
The peak absorbed power during the laser pulse is:
Peak absorbed power
Pabs,peak = 800 W
5. Why Average Power Alone Is Not Enough
Two welding processes can have the same average power but completely different thermal cycles.
For example:
Case A
gives:
Case B
also gives:
The average power is identical.
However, Case A produces short periods of very high heat input followed by cooling periods.
Case B produces continuous heating.
Therefore, the two cases can produce different:
- Peak temperatures
- Fusion-zone dimensions
- Cooling rates
- HAZ dimensions
- Thermal gradients
- Solidification behavior
- Residual stresses
- Distortion
Numerical studies of pulsed laser welding show that pulse width and frequency can significantly change temperature distribution and penetration.
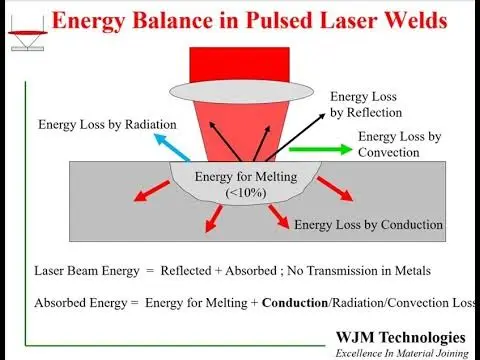
6. Time-Dependent Representation of a Pulsed Laser
For an ideal rectangular pulse, define the laser power as:
where:
and the pattern repeats every:
A convenient mathematical representation is:
where:
This is the basic pulse function that should be incorporated into a moving laser heat source.
A pulsed laser can therefore be considered as:
where () describes the spatial laser distribution and (g(t)) controls whether the laser is ON or OFF.
7. Pulsed Moving Gaussian Heat Source
For a laser welding model, a Gaussian distribution is often used to describe the spatial energy distribution.
For a surface heat source:
where:
- () = absorption efficiency
- () = peak laser power
- () = laser beam radius
- () = laser position
- () = pulse function
The laser position for straight welding can be written as:
where (v) is welding speed.
Therefore:
This equation contains both essential parts of the pulsed laser:
spatial distribution + temporal pulse modulation.
8. Volumetric Heat Source for Laser Welding
If you use a body heat flux in Abaqus, your heat source must have units of energy per volume per time.
For SI units:
A simple volumetric Gaussian source can be written as:
where (d) is an effective penetration depth.
The exact spatial model should be selected according to the welding regime.
A shallow conduction-mode weld can often be represented with a surface or shallow volumetric source.
A deep-penetration keyhole weld may require a more sophisticated model because vaporization, recoil pressure, multiple reflections, and melt-pool flow can become important. Numerical pulsed-laser studies have explicitly included effects such as recoil pressure, thermocapillary flow, vaporization, and multiple beam reflections for keyhole modeling.
9. Pulse Function in Abaqus DFLUX
For an Abaqus/Standard transient heat-transfer analysis, DFLUX can define a nonuniform heat flux as a function of position, time, temperature, element number, and integration point. Abaqus calls the subroutine at the flux integration points.
For a body heat flux, FLUX(1) has units:
which becomes:
when using SI units.
The pulse should therefore be included directly in the heat-source equation.
For example:
      t = TIME(2)

      period = 1.0D0/frequency

      phase = MOD(t,period)

      IF (phase .LT. pulse_width) THEN
         pulse = 1.0D0
      ELSE
         pulse = 0.0D0
      END IF
Then:
FLUX(1) = q_gaussian*pulseDuring the ON period:
pulse = 1During the OFF period:
pulse = 0This produces a true pulsed heat source.
10. Do Not Use a DO Loop to Represent Time
A common mistake in DFLUX is attempting something like:
DO i=1,TIME(2)This is not how Abaqus time should be handled.
TIME(2) is a real-valued Abaqus time variable.
Use:
t = TIME(2)and calculate the pulse phase directly:
phase = MOD(t,period)Then determine whether the laser is ON or OFF.
Abaqus already calls DFLUX at the current integration-point time. There is no need to manually loop through previous time values.
11. Recommended DFLUX Structure
A clean pulsed moving laser subroutine should have five sections:
1. Read Abaqus time
       ↓
2. Calculate laser position
       ↓
3. Calculate pulse state
       ↓
4. Calculate spatial heat source
       ↓
5. Return FLUX(1)
Conceptually:
      t = TIME(2)

      xlaser = x0 + velocity*t

      period = 1.0D0/frequency
      phase  = MOD(t,period)

      IF (phase .LT. pulse_width) THEN
         pulse = 1.0D0
      ELSE
         pulse = 0.0D0
      END IF

      q = spatial_heat_source

      FLUX(1) = q*pulse
This structure is much easier to debug than embedding time loops inside DFLUX.
12. DFLUX and Abaqus Amplitude
There is an important Abaqus-specific issue here.
When you define a nonuniform distributed flux through DFLUX, Abaqus ignores amplitude references associated with that nonuniform distributed flux. Therefore, if the pulse is controlled by DFLUX, implement the pulse function inside the subroutine rather than assuming an Abaqus amplitude will modulate the DFLUX value.
In other words, for a user-defined pulsed laser:
DFLUX
   │
   ├── laser position
   ├── Gaussian distribution
   ├── peak power
   └── pulse function
is preferable to relying on a separate amplitude curve.
13. Pulse Width and Frequency
The two most important temporal parameters are usually:
- Pulse width
- Frequency
Pulse width determines how long the laser remains ON.
Frequency determines how frequently the pulse repeats.
For example:
| Peak power | Pulse width | Frequency | Duty cycle |
| 1000 W | 1 ms | 100 Hz | 10% |
| 1000 W | 2 ms | 100 Hz | 20% |
| 1000 W | 5 ms | 100 Hz | 50% |
| 1000 W | 8 ms | 100 Hz | 80% |
For the same peak power, increasing pulse width increases average energy input.
At constant pulse width, increasing frequency also increases average power.
14. Pulse Energy Is Often More Useful Than Peak Power
For comparing experiments, pulse energy is often a better parameter than peak power alone.
For example:
Pulse A
Pulse B
Both deliver the same energy per pulse.
However, they do not necessarily produce the same peak temperature because the energy is delivered at different rates.
Therefore, when analyzing pulsed welding, track both:
and:
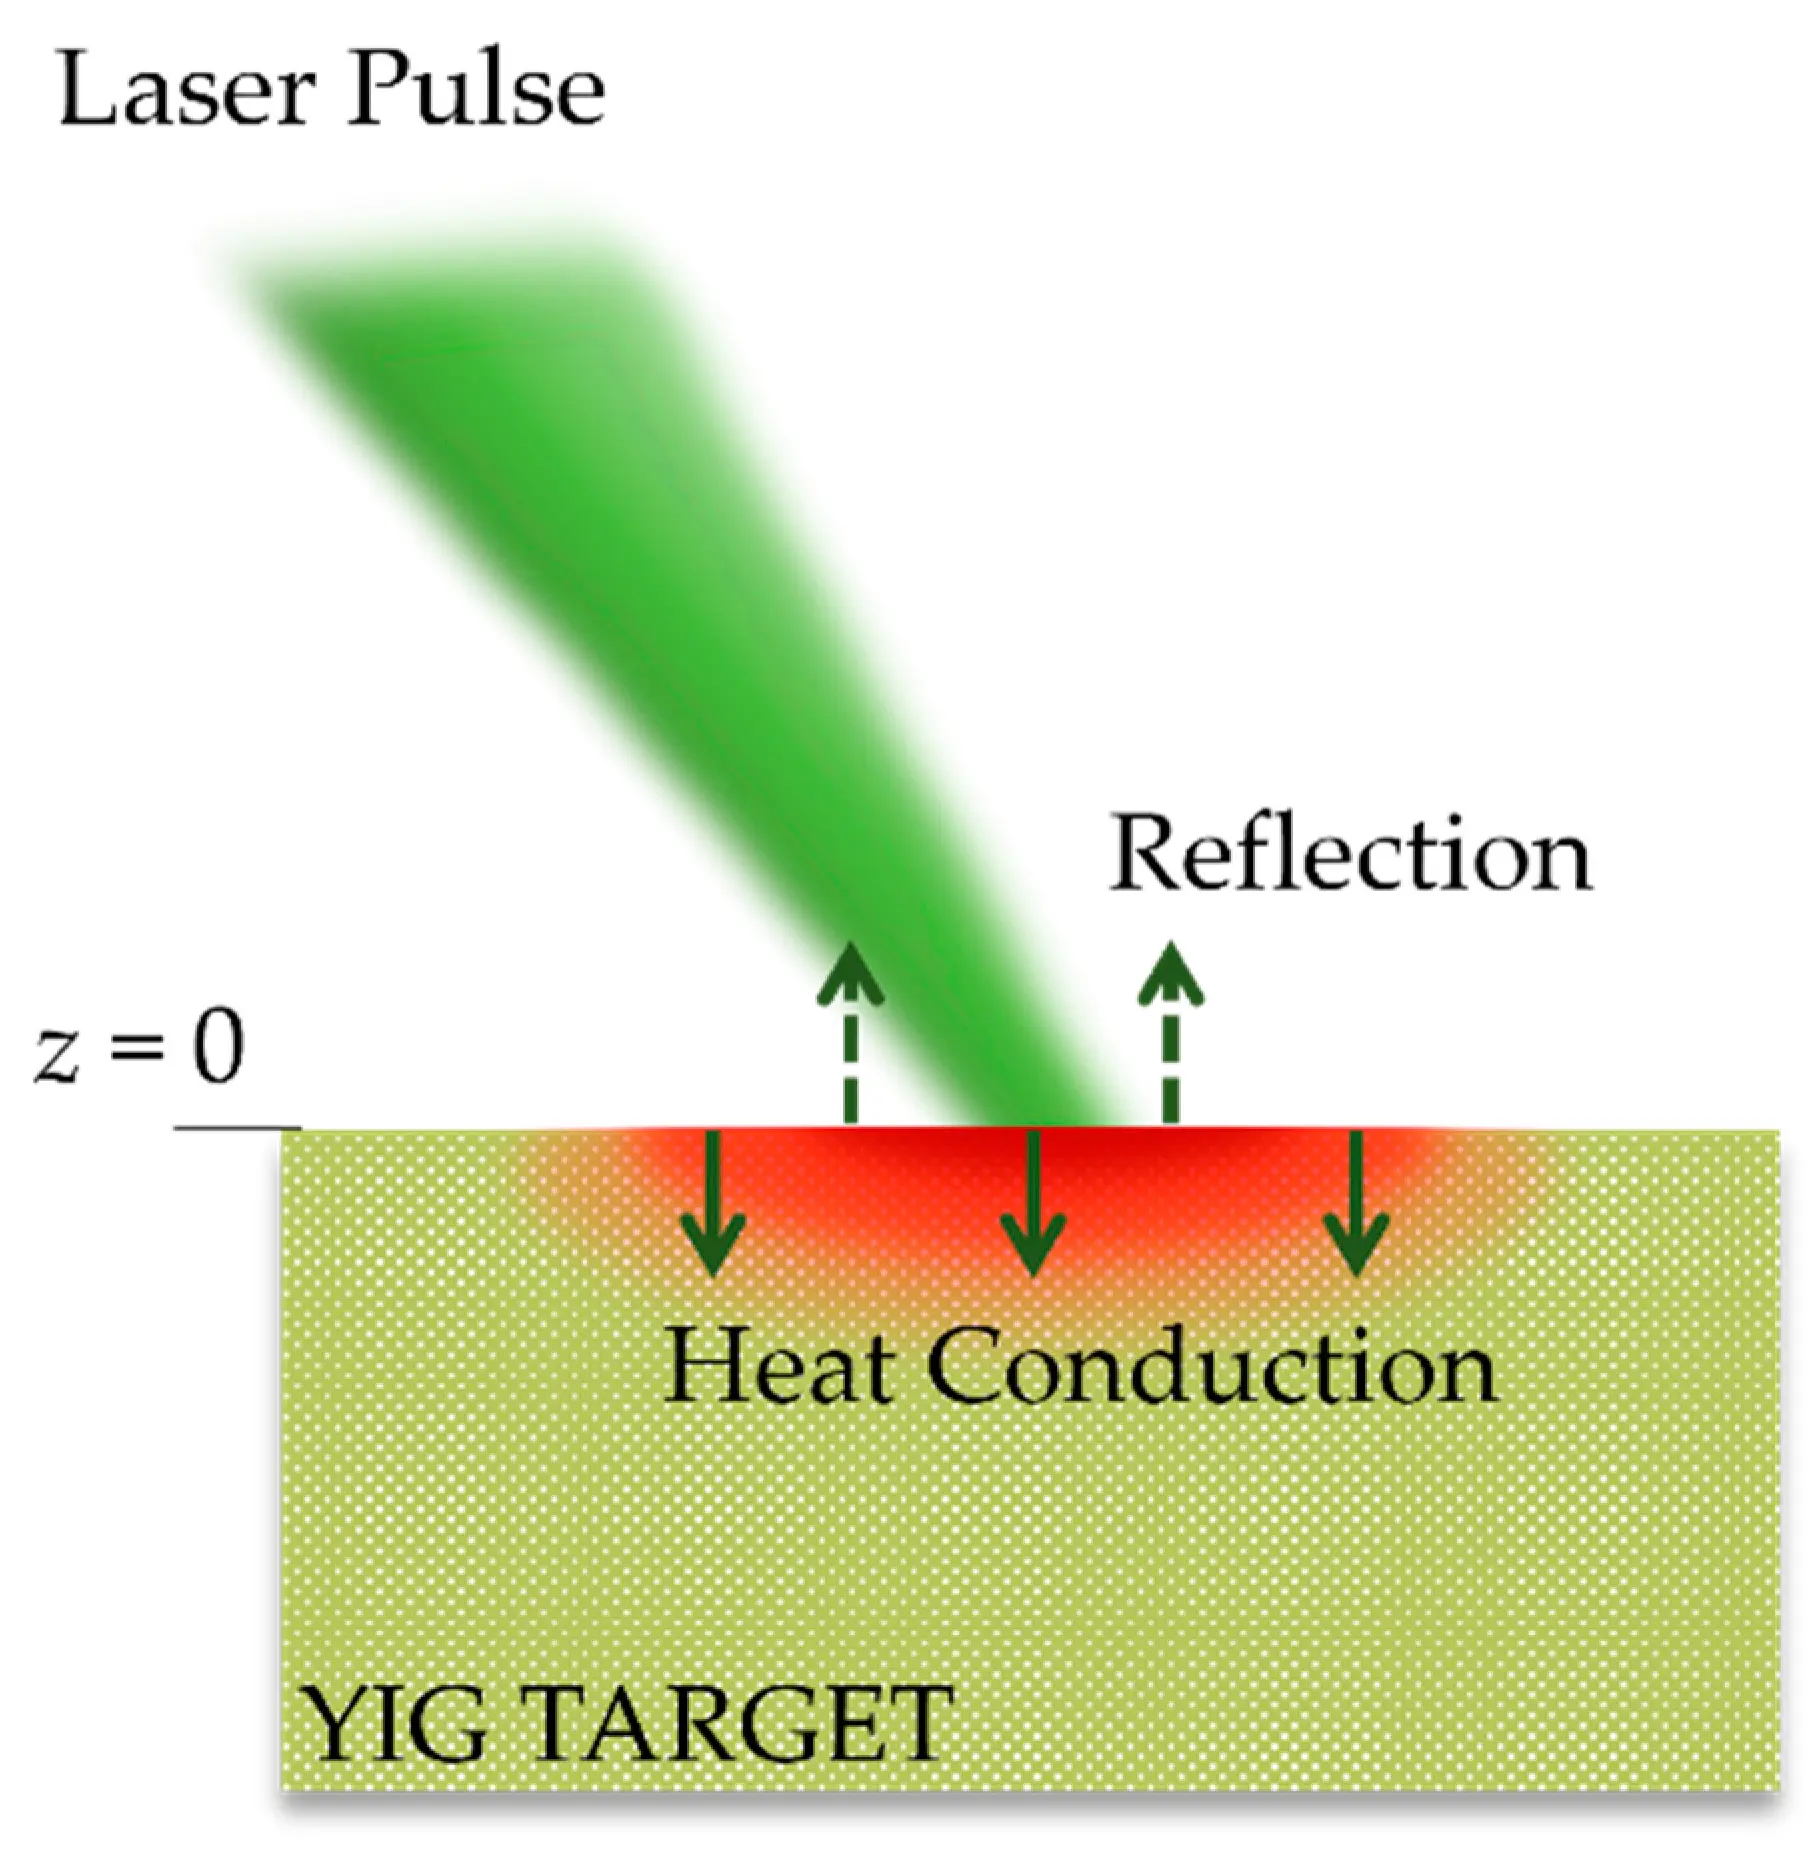
15. Heat Input per Unit Length
For a moving laser, average linear heat input can be approximated as:
where:
- (H) = absorbed energy per unit length
- () = average laser power
- (v) = welding speed
Using:
gives:
For the example:
then:
or:
This is a useful quantity for comparing different welding conditions.
However, equal linear heat input does not guarantee equal weld geometry because pulsed heating changes the instantaneous thermal cycle.
16. Thermal Cycle in Pulsed Welding
A pulsed weld produces repeated heating and cooling cycles.
A typical point near the weld can experience:
Temperature

   ↑
   │       /\        /\        /\
   │      /  \      /  \      /  \
   │     /    \    /    \    /    \
   │____/      \__/      \__/      \____
   │
   └──────────────────────────────────→ time
Each pulse can produce:
- Rapid heating
- Melting
- Peak temperature
- Laser OFF
- Cooling
- Possible solidification
- Reheating by the next pulse
This repeated thermal cycling is one of the defining characteristics of pulsed welding.
17. Thermal Properties Must Be Temperature Dependent
For a realistic numerical model, do not use room-temperature thermal properties throughout the welding cycle.
At minimum, use:
For thermo-mechanical analysis, also use:
Temperature-dependent material properties become especially important when the weld pool approaches the melting range.
Numerical pulsed-laser welding studies have used temperature-dependent thermophysical properties when predicting transient temperature fields and weld dimensions.
18. Melting and Latent Heat
If the predicted temperature reaches the melting range, include latent heat.
For a material with:
and:
the latent heat can be incorporated over the melting interval.
One practical approach is to use an effective heat capacity:
within the solidus–liquidus interval.
Here:
- (L) = latent heat of fusion
- () = solidus temperature
- () = liquidus temperature
For a laser-welding model, this treatment is generally more appropriate than ignoring latent heat when the objective includes fusion-zone prediction.
19. Pulse Frequency and Heat Accumulation
Frequency controls how much the material cools between pulses.
At high frequency:
becomes small.
The material may therefore remain hot when the next pulse arrives.
At low frequency, the material has more time to cool.
This produces two different regimes.
High frequency
Pulse  Pulse  Pulse  Pulse
 /\     /\     /\     /\
/  \___/  \___/  \___/  \__
The temperature baseline can progressively increase.
Low frequency
Pulse       Pulse       Pulse
 /\          /\          /\
/  \________/  \________/  \____
The material experiences stronger individual heating and cooling cycles.
The effect of frequency is not simply a change in average power. Numerical studies have shown changes in penetration and temperature distribution when pulse frequency is varied.
20. Pulse Width Controls Peak Thermal Response
At a fixed pulse energy:
reducing pulse width requires higher peak power.
For example:
2 J pulse
Case A:
Case B:
Both deliver:
but Case B deposits the energy twice as quickly.
Therefore, the peak temperature can be substantially different even though the pulse energy is identical.
21. Choosing Pulse Parameters for Simulation
A useful parameter study should not vary every variable randomly.
Start with a baseline case.
For example:
| Parameter | Baseline |
| Peak power | 1000 W |
| Frequency | 100 Hz |
| Pulse width | 2 ms |
| Duty cycle | 20% |
| Welding speed | 10 mm/s |
| Efficiency | 0.8 |
| Beam radius | 0.5 mm |
Then vary one parameter at a time.
Study A ; Pulse width
Keep:
constant.
Test:
Study B ; Frequency
Keep:
constant.
Test:
Study C ; Peak power
Keep:
constant.
Test:
This separates the effects of each parameter.
22. Mesh Requirements for Pulsed Welding
Pulsed welding creates a rapidly changing heat source.
Therefore, both mesh size and time increment matter.
The mesh must resolve the laser spot and expected fusion zone.
For example, if:
using elements several millimeters wide is inappropriate for resolving the heat source.
A practical starting point is to have multiple elements across the beam diameter.
The time increment must also resolve the pulse.
If:
using only one increment over the entire pulse is generally too coarse.
You need several increments within the ON period and enough resolution during the OFF period to capture cooling.
22. Time-Step Recommendation
For a pulse width:
[
a reasonable starting point is to allow approximately:
increments during the pulse.
For example:
as an initial numerical test.
This is not a universal rule. You should perform a time-step sensitivity study.
Compare:
- Maximum temperature
- Fusion-zone width
- Fusion-zone depth
- Temperature history
for progressively smaller increments.
24. Boundary Conditions
A pulsed laser simulation should include realistic heat losses.
The most common mechanisms are:
Convection
Radiation
where absolute temperature must be used for the radiation equation.
For high-temperature welding, radiation can become significant because of the () dependence.
25. Initial Temperature
The initial workpiece temperature should be specified explicitly.
For room-temperature welding:
For preheated welding:
The initial temperature affects:
- Peak temperature
- Cooling rate
- HAZ
- Thermal gradients
- Residual stress
26. Welding Speed and Pulse Spacing
The distance traveled by the laser during one pulse period is:
For example:
and:
f=100;Hz
gives:
Therefore, consecutive pulses are separated by approximately 0.1 mm along the welding direction.
This quantity is extremely useful when designing the simulation mesh.
The ratio between pulse spacing and beam diameter helps determine whether the process produces:
- strongly separated individual spots
- overlapping spots
- nearly continuous heating
27. Pulse Overlap
For a beam diameter (d_b), a simple spatial overlap estimate is:
for a straight path under a simplified geometric interpretation.
For example:
gives:
This means the pulses strongly overlap spatially.
However, pulse overlap should not be used as a substitute for the actual transient thermal simulation. The temperature field depends on heat conduction, pulse energy, material properties, and boundary conditions.
28. Abaqus Model Architecture
For a practical Abaqus laser-welding model, a useful workflow is:
Geometry
   ↓
Material properties
   ↓
Temperature-dependent k, Cp, ρ
   ↓
Mesh
   ↓
Initial temperature
   ↓
Convection + radiation
   ↓
Moving pulsed DFLUX
   ↓
Transient heat-transfer analysis
   ↓
Temperature field
   ↓
Fusion-zone prediction
   ↓
Thermo-mechanical analysis
For an uncoupled thermal analysis, temperature-dependent thermal properties are the primary material inputs.
For residual-stress analysis, transfer the temperature history into a mechanical analysis.
29. Recommended DFLUX Logic
For a moving pulsed laser, use this sequence:
t = TIME(2)

xlaser = x0 + velocity*t

period = 1.0D0/frequency

phase = MOD(t,period)

IF (phase .LT. pulse_width) THEN
    pulse = 1.0D0
ELSE
    pulse = 0.0D0
END IF

q = spatial_heat_source

FLUX(1) = q*pulse
This is preferable to using an artificial time loop.
Abaqus supplies the current time to DFLUX, so the subroutine should evaluate the heat source at that time.
30. Common DFLUX Errors in Pulsed Welding
Error 1 ; Using average power as peak power
Wrong:
when the laser actually has a duty cycle below 100%.
Correct:
Error 2 ; Forgetting pulse modulation
Using:
FLUX(1)=q_gaussiancreates a continuous laser.
For pulsed welding:
FLUX(1)=q_gaussian*pulseis required.
Error 3 ; Using a DO loop over TIME(2)
Avoid:
DO i=1,TIME(2)TIME(2) is real-valued and represents Abaqus time.
Use:
t=TIME(2)instead.
Error 4 ; Incorrect units
A body heat flux must have units:
]
when SI units are used.
A surface heat flux has units:
Do not use a surface Gaussian equation directly as a volumetric body heat source.
Abaqus explicitly distinguishes these two load types.
Error 5 ; Laser moves outside the model
If:
make sure the resulting laser position remains within the model during the welding step.
Error 6 ; Pulse width is smaller than the time increment
If:
but:
the numerical model cannot properly resolve the pulse.
Error 7 ; Laser spot is smaller than the mesh
A highly concentrated heat source requires sufficient spatial resolution.
31. Energy Conservation Check
One of the best ways to validate a pulsed DFLUX implementation is to calculate the expected total energy.
For a welding duration (t_w):
or:
The absorbed energy should be approximately:
Your Abaqus model should produce an energy balance consistent with this value, allowing for heat losses and numerical effects.
This is often a more reliable debugging method than looking only at the maximum temperature.
32. How to Validate a Pulsed Welding Simulation
Do not validate the model using only the maximum temperature.
Compare the predicted and experimental:
Thermal quantities
- Peak temperature
- Temperature history
- Heating rate
- Cooling rate
Weld geometry
- Fusion-zone width
- Fusion-zone depth
- Weld cross-sectional area
- HAZ width
Mechanical quantities
- Residual stress
- Distortion
- Plastic strain
A model that reproduces the maximum temperature but predicts the wrong fusion-zone geometry is not adequately validated.
33. Recommended Results to Extract in Abaqus
For a pulsed laser welding model, extract:
Temperature
Heat flux
Temperature history
Create history output at points:
- Weld centerline
- Fusion boundary
- HAZ
- Base metal
Fusion zone
Define an isotherm near the liquidus temperature.
For example, if:
the region above approximately this temperature can be used as an initial estimate of the molten region.
The exact criterion should be consistent with the material and melting model.
34. Practical Parameter Relationships
The most useful relationships are:
These equations form the basic parameter framework for pulsed laser welding.
35. Pulsed Welding vs Continuous-Wave Welding
The key difference is not simply that pulsed welding has “less heat.”
The important difference is the temporal distribution of the energy.
| Feature | Continuous wave | Pulsed |
| Laser power | Continuous | Periodic |
| Peak power | Usually equal to operating power | Can be much higher than average |
| Average power | Operating power | Lower than peak power |
| Heating | Continuous | Repeated |
| Cooling between pulses | Minimal | Can be significant |
| Peak temperature | Depends on power | Strongly affected by pulse width |
| Thermal cycling | Relatively smooth | Strongly periodic |
| Pulse energy | Not applicable | Important parameter |
| Frequency | Not applicable | Important parameter |
| Duty cycle | ~100% | Usually <100% |